ABS is the default choice for product housings. It's cost-effective, easy to process, and looks good. But what makes it work — and when should you consider something else?
Here's what you need to know.
What Is ABS?
ABS is made from three monomers: acrylonitrile for strength and chemical resistance, butadiene for toughness, and styrene for rigidity and processability.
Change the ratio, and you change the performance. That‘s why there are so many grades — some stiffer, some tougher, some more heat-resistant. A general-purpose grade behaves very differently from a flame-retardant or plating grade.
What ABS Is Good At
It balances stiffness and toughness. It holds its dimensions under stress. It takes color, printing, and chrome plating well.
For most indoor products, these properties are enough.
Where ABS Falls Short
Heat resistance is limited — typically below 60°C. That rules out applications near heat sources or in high-temperature environments.
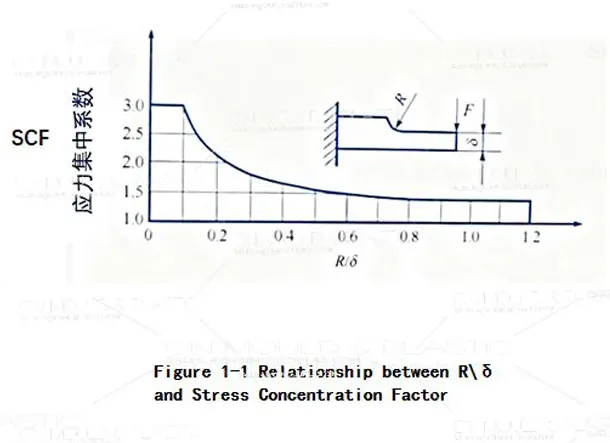
It's sensitive to stress cracking, especially around bosses and sharp corners, where molded-in stress concentrates.
And it requires drying before processing. 80–90°C for 2–4 hours. Skip it, and you'll get silver streaks and bubbles on the part surface.
ABS Can Be Blended for Better Performance
PC/ABS improves heat resistance, UV resistance, and flow. It's the go-to alloy for medical device housings, automotive interiors, and electronics enclosures that need more than standard ABS can deliver.
PBT/ABS improves chemical resistance (including gasoline) and dimensional stability at high temperatures. In automotive interiors, it's replacing ABS, PP, and PC/ABS because its matte surface better replicates textile appearance.
How We Process ABS
ABS is one of the more "friendly" materials to process — but it still requires the right approach.
Drying is non-negotiable. 80–90°C for 2–4 hours. Skip it, and you get silver streaks and bubbles.
Injection temperature must be controlled within a narrow window. Too low, and the cavity won't fill. Too high, and the material degrades.
Mold design needs to account for the specific grade. Shrinkage, draft angle, and gate location all vary between general-purpose, flame-retardant, and plating grades.
Pre-treatment for plating, painting, or printing directly affects adhesion. A poorly prepared surface will fail even with the right process parameters.
 English
 français
 Deutsch
 Español
 italiano
 русский
 português
 العربية
 dansk
 Suomi
 Svenska
 norsk